Food Engineering logo
search
cart
facebook twitter linkedin youtube
  • Sign In
  • Create Account
  • Sign Out
  • My Account
Food Engineering logo
  • NEWS
    • Latest Headlines
    • Manufacturing News
    • People & Industry News
    • Plant Openings
    • Recalls
    • Regulatory Watch
    • Supplier News
  • PRODUCTS
    • New Plant Products
    • New Retail Products
  • TOPICS
    • Alternative Protein
    • Automation
    • Cannabis
    • Cleaning | Sanitation
    • Cross-Functional Food Innovation
    • Fabulous Food Plants
    • Food Safety
    • Maintenance Strategies
    • OEE
    • Packaging
    • Sustainability
    • More
  • EXCLUSIVES
    • Plant Construction Survey
    • Plant of the Year
    • Sustainable Plant of the Year
    • State of Food Manufacturing
    • Top 100 Food & Beverage Companies
  • MEDIA
    • Podcasts
    • Videos
    • Webinars
    • White Papers
  • FOOD MASTER
  • EVENTS
    • Food Automation & Manufacturing Symposium and Expo
    • Industry Events
  • RESOURCES
    • Newsletter
    • Custom Content & Marketing Services
    • FE Store
    • Government Links
    • Industry Associations
    • Market Research
    • Sponsor Insights
    • Classified Ads
  • EMAGAZINE
    • eMagazine
    • Archive Issue
    • Advertise
  • SIGN UP!
AutomationDry Processing

Dry Processing Technology

Milk Specialties uses manufacturing intelligence to improve operations

Manufacturing intelligence helps Milk Specialties Global keep products “moo-ving.”

By Casey Laughman
FactoryTalk VantagePoint software

A screenshot of the Rockwell Automation FactoryTalk VantagePoint manufacturing intelligence software. Source: Rockwell Automation.
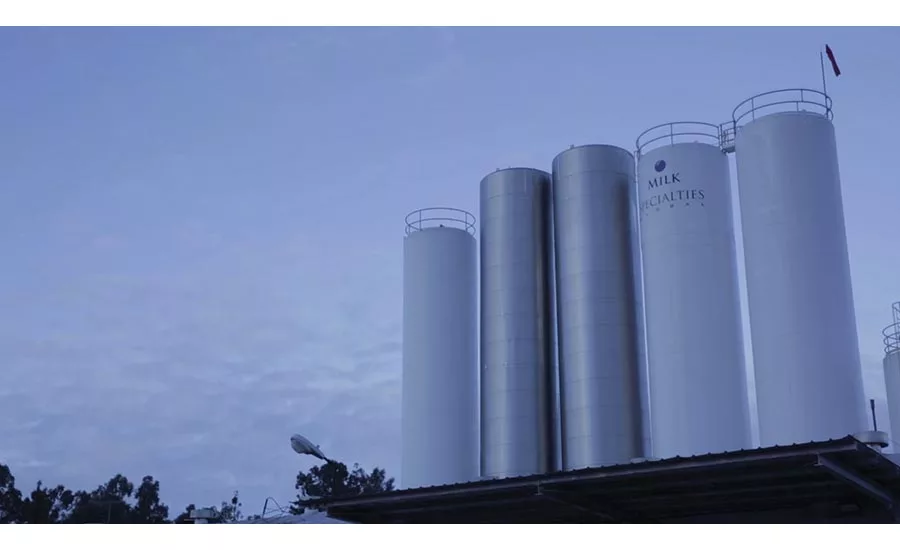
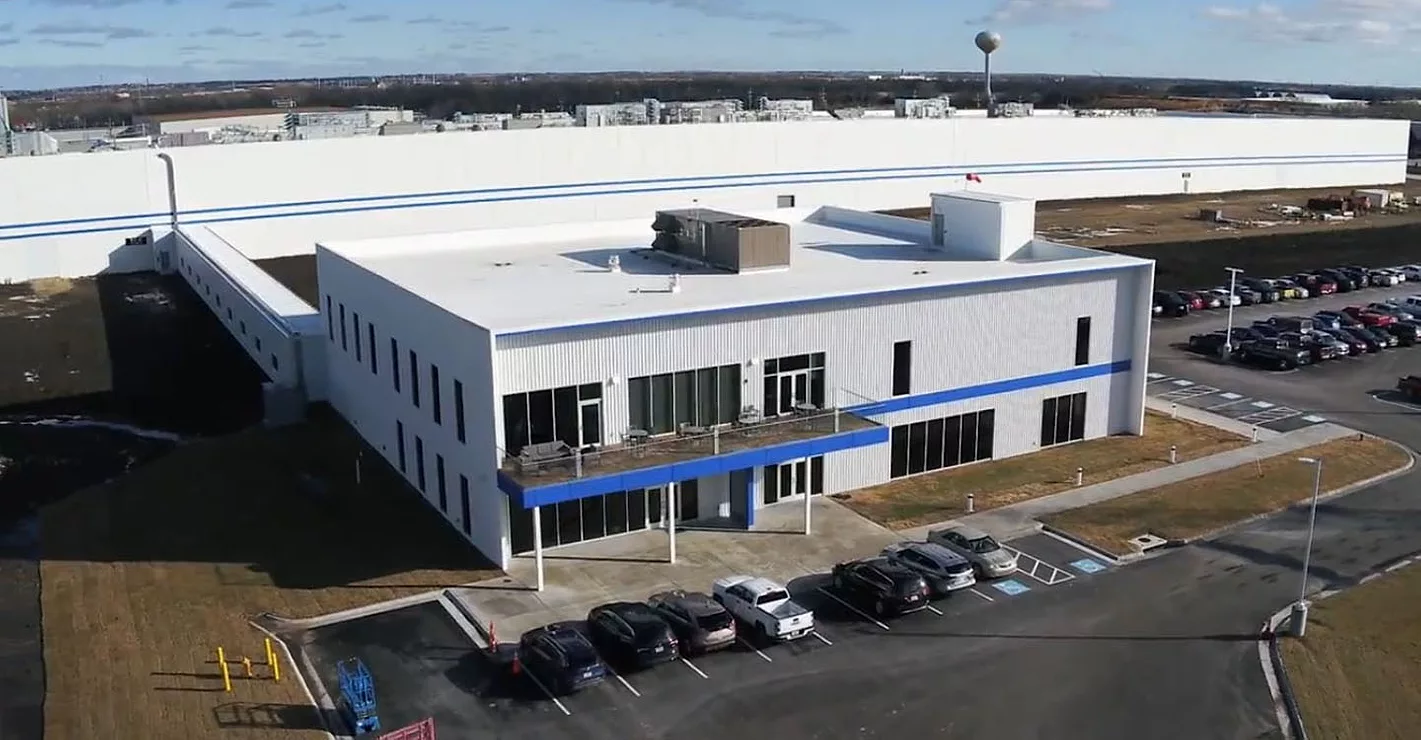
Milk Specialty Global's Visalia facility

An exterior shot of Milk Specialty Global’s Visalia, CA facility. Source: Rockwell Automation.

FactoryTalk VantagePoint software
Milk Specialty Global's Visalia facility
August 21, 2017

Think about dairy, and you likely conjure up familiar grocery staples like milk, cheese and butter. But the proteins found in raw dairy products also serve as key ingredients for a wide range of health and nutrition products.

Milk Specialties Global is a major supplier of these proteins, with 10 manufacturing facilities located throughout the Midwest and in California. The Minnesota-based company processes raw milk and whey into a broad portfolio of ingredients, including milk proteins, whey proteins and specialty proteins.

These ingredients are then shipped to customers that use them in food and beverage products ranging from coffee creamers and baking goods to processed cheeses and Greek yogurts. They are also a primary ingredient in high-demand, sports-nutrition, weight-loss products, such as protein powders, protein shots and meal-replacement bars. And they are used in a variety of animal-nutrition products, including milk replacers, energy boosters and nutritional supplements.

Milk Specialties has rapidly grown in recent years to keep up with market demand. The company of only about 800 employees is today nearing $1 billion in annual revenue. To help meet high demand, the company recently made investments in manufacturing intelligence to achieve real-time analytics and insights into its operations to drive improvements in production processes.

Despite the tremendous variations that can occur in the raw ingredient input streams that the company receives, it still must deliver consistent-quality output streams.

For its human nutrition products, the raw, dairy-product stream is separated with state-of-the-art membrane technologies—which allows the isolated proteins to remain in their native state. From there, the stream is sent through a dryer and finally to the packaging line. Identifying and improving inefficient processes in these operations were challenging. The facilities’ production control systems were data silos, with little ability to track or compare data over time. And the reporting capabilities that were in place were outdated and labor intensive.

For example, tracking the clean-in-place (CIP) chemical usage involved workers downloading data from a machine into a Microsoft Word document and then manually entering that data into a spreadsheet to create a graph. This not only took time, it also restricted workers’ abilities to view data quickly and within multiple contexts to truly understand CIP chemical usage.

When the company inherited a legacy, historian software system with an acquired production facility in Visalia, CA, Mike Calva, corporate programmer and analyst for Milk Specialties Global, saw an opportunity to do more with production data.

“The historian was only being used for compliance,” says Calva. “It basically worked in the background, and we weren’t getting anything out of it from an operations perspective. But we knew the potential was there. We wanted something for production that could help us discover the ‘art of the possible’ in our operations.”

Milk Specialties drew up plans to begin rolling out manufacturing intelligence systems across its three primary human nutrition facilities. These included the Visalia location, as well as facilities in Fond du Lac, WI and Mountain Lake, MN.

The company chose FactoryTalk VantagePoint EMI enterprise manufacturing intelligence software from Rockwell Automation, which can integrate a variety of production and business data into a single information-management, analytics and decision-support system. Within Milk Specialties’ operations, the software collects, correlates and displays real-time process, business and laboratory data.

The system was first implemented at the Fond du Lac facility. In the process of rolling out the EMI software at the Visalia facility, the scope grew as users kept discovering new opportunities for using it.

“An idea for using the software to create in-plant scoreboards came about during the implementation,” Calva says. “Our chief operating officer was the driving force behind that. He wanted everyone on the plant floor to have visibility—to always know if we are winning or losing based on our performance data—and then have the tools to dig into the issue, investigate the root cause of underperformance and fix it.”

At the Visalia facility, tailored scoreboards were placed in three key production areas: separation, filtration and drying. A fourth scoreboard, displaying plant-wide operations, was placed in the facility’s front office.

The scoreboard in each production area displays plant summary data, such as throughput, as well as data relevant to workers in that specific location. For example, workers in the separation area can view the fat volume in the skim stream or the temperature in the pasteurizing process, while workers in the dryer area can view evaporation levels and outputs to the bagging line.

The EMI software has established a decision-making process that is based on data and can be applied to any one of the facilities. For instance, when process engineers at the Fond du Lac facility wanted to add a new mid-wash process to perform an additional flush between batch runs, the new system showed significant yield improvements following the change.

The software also helped resolve an issue with the dryer in the Visalia plant. After reviewing data on the operators’ activities, including seeing down to the level of operators’ sequence of actions, it was learned that operators were not starting up and shutting down the equipment in the right sequence.


For more information:

Rockwell Automation, 414-486-5800,
sales@rockwellautomation.com, www.rockwellautomation.com.

KEYWORDS: data acquisition nutrition

Share This Story

Looking for a reprint of this article?
From high-res PDFs to custom plaques, order your copy today!

Casey laughman0031

Casey Laughman is the former Editor in Chief of Food Engineering magazine. He has almost two decades’ experience as a writer and editor for mainstream and trade publications. He spent several years as a writer and editor for two news services before becoming the editor of a legal publication and managing editor of a trade magazine that covered the commercial facilities market.

Recommended Content

JOIN TODAY
to unlock your recommendations.

Already have an account? Sign In

  • Bread going through conveyor belt in manufacturing plant.

    The State of Food Manufacturing in 2026

    Food and beverage manufacturers encounter significant...
    Sustainability
    By: Alyse Thompson-Richards
  • FE Top100 Food & Beverage Companies hero, gold lettering with black background.

    FOOD ENGINEERING’s 2026 Top 100 Food and Beverage Companies

    See where the world’s leading food and beverage companies...
    Manufacturing News
    By: Alyse Thompson-Richards
  • CJ Schwan’s Salina facility.

    Recipe for Growth: How CJ Schwan’s Powers Pizza Production with People and Automation

    Blending advanced automation with purposeful design, this...
    Plant of the Year
    By: Alyse Thompson-Richards
Manage My Account
  • eMagazine
  • Newsletter
  • Online Registration
  • Manage My Preferences
  • Customer Service

More Videos

Sponsored Content

Sponsored Content is a special paid section where industry companies provide high quality, objective, non-commercial content around topics of interest to the Food Engineering audience. All Sponsored Content is supplied by the advertising company and any opinions expressed in this article are those of the author and not necessarily reflect the views of Food Engineering or its parent company, BNP Media. Interested in participating in our Sponsored Content section? Contact your local rep!

close
  • Illustration of businessman standing in the middle of a large scale, balancing between two green dollar signs at each end, one larger than the other. Blue background with very small white clouds.
    Sponsored by3-A Sanitary Standards, Inc.

    6 Questions: Before You Buy Food Processing Equipment

  • Construction crews use aerial lifts to install insulated wall panels inside an industrial facility.
    Sponsored byBurns & McDonnell

    Food Manufacturing’s Growth Calls for Integrated Project Delivery

  • Close-up of a group of freshly baked stuffed empanadas being transferred onto a conveyor belt.
    Sponsored byDorner

    Smarter Line Design Improves Food Manufacturing Efficiency and Throughput

Popular Stories

Bread going through conveyor belt in manufacturing plant.

The State of Food Manufacturing in 2026

Illustration of businessman standing in the middle of a large scale, balancing between two green dollar signs at each end, one larger than the other. Blue background with very small white clouds.

6 Questions: Before You Buy Food Processing Equipment

Maple Leaf Foods photo

Maple Leaf Foods to Consolidate Plant Protein Production

An image of baked bread on a conveyor belt with text promoting the 2026 State of Food Manufacturing report.

Events

January 1, 2030

Webinar Sponsorship Information

For webinar sponsorship information, visit www.bnpevents.com/webinars or email webinars@bnpmedia.com.

View All Submit An Event

Products

Food Process Engineering and Technology, 3E

Food Process Engineering and Technology, 3E

Combining scientific depth with practical usefulness, this book serves as a tool for graduate students as well as practicing food engineers, technologists and researchers looking for the latest information on transformation and preservation processes as well as process control and plant hygiene topics.

See More Products
Promo for the 2027 Plant of the Year Award


CHECK OUT OUR NEW ESSENTIAL TOPICS

Alternative Protein Automation Cleaning/Sanitation Fabulous Food Plants

Food Safety Maintenance Strategies OEE

Packaging Sustainability

Related Articles

  • Brewer taps manufacturing intelligence to enhance its process

    See More
  • Manufacturing survey finds cloud-based systems improve operations

    See More
  • Key blueberry

    Blueberry processor uses digital sorter to improve defect removal

    See More

Related Products

See More Products
  • Cleaning-in-Place: Dairy, Food and Beverage Operations, 3rd Edition

See More Products

Events

View AllSubmit An Event
  • October 31, 2017

    Total Productive Maintenance (TPM): Strategies to Improve Your F&B Operations

    ON DEMAND: Tetra Pak’s expertise is rooted in deep experience with our own factories as well as our work on a diverse range of global projects. In this webinar, we’ll share strategies tailored for the food and beverage industry, including how to improve business performance by understanding losses, implementing sustainable improvements and achieving a higher, more flexible and predictable production.
View AllSubmit An Event
×

Elevate your expertise in food engineering with unparalleled insights and connections.

Get the latest industry updates tailored your way.

JOIN TODAY!
  • RESOURCES
    • Advertise
    • Contact Us
    • Food Master
    • Store
    • Want More
  • SIGN UP TODAY
    • Create Account
    • eMagazine
    • Newsletter
    • Customer Service
    • Manage Preferences
  • SERVICES
    • Marketing Services
    • Reprints
    • Market Research
    • List Rental
    • Survey/Respondent Access
  • STAY CONNECTED
    • LinkedIn
    • Facebook
    • YouTube
    • X (Twitter)
  • PRIVACY
    • PRIVACY POLICY
    • TERMS & CONDITIONS
    • DO NOT SELL MY PERSONAL INFORMATION
    • PRIVACY REQUEST
    • ACCESSIBILITY

Copyright ©2026. All Rights Reserved BNP Media, Inc. and BNP Media II, LLC.

Design, CMS, Hosting & Web Development :: ePublishing