Pumps/Vacuums/Weighing
Alfa Laval Debuts MaxiLobe Rotary Lobe Pumps
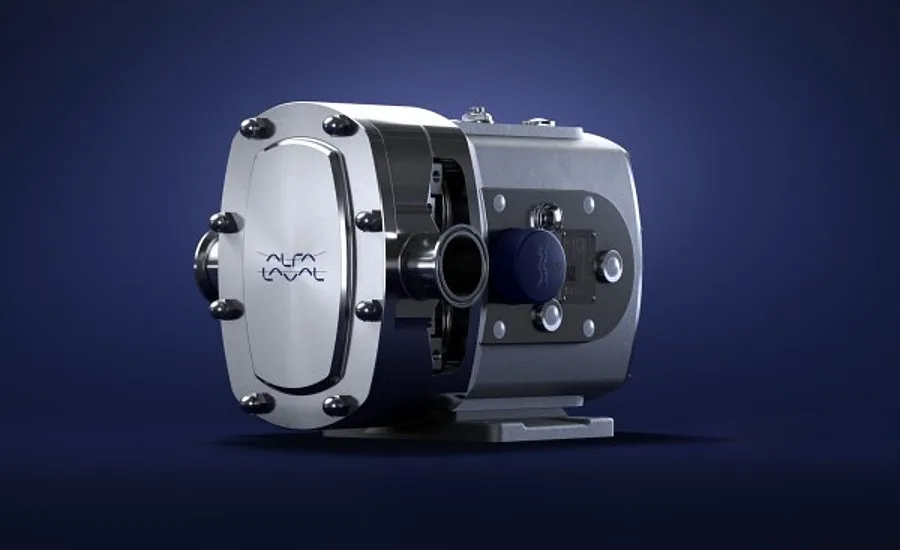
Alfa Laval is introducing MaxiLobe rotary lobe pumps, which are positive displacement pumps designed to improve volumetric efficiency, with the potential to reduce capital investment and deliver energy savings.
Manufacturers in the dairy, food and beverage industries are under constant pressure to improve efficiency, maximize uptime and reduce the total cost of ownership. The Alfa Laval MaxiLobe and MaxiLobe UltraPure pump ranges address these priorities through higher volumetric efficiency, a broader operating envelope, enhanced assurance and simpler service.
“For decades, our rotary lobe pumps have been widely used in hygienic and high-purity processing where reliability and predictable performance are essential,” says Russ Kelly, portfolio manager, pumps at Alfa Laval. “MaxiLobe builds on that legacy with improved hygienic design across a wider operating range, enabling smaller pumps to achieve the same duty at lower speeds. Lower speeds reduce shear, helping improve operating efficiency and safeguard shear-sensitive products.”
MaxiLobe and MaxiLobe UltraPure pumps aim to optimize capital investment with a broad flow and pressure envelope. Additionally, by enabling a smaller pump to be selected for the required duty in suitable applications, MaxiLobe can reduce equipment and installation costs, including the associated electrical equipment. This reduces the need for oversizing while maintaining operational flexibility.
Upgrades are equally straightforward. Key porting dimensions match those of all Alfa Laval SRU pumps and most SX and SX UltraPure models, allowing replacement without modifying existing pipework. Under defined operating conditions, MaxiLobe delivers at least 5% higher flow rates than the equivalent SRU model, improving process capacity without increasing footprint or installation complexity.
MaxiLobe and MaxiLobe UltraPure pumps can deliver the required flow rates at lower operating speeds, helping reduce energy consumption and electricity costs. In many applications, this can result in energy savings of more than 25%. Operating the pumps at lower speeds also reduces shear on sensitive products that may be damaged when operating at higher speeds. By reducing mechanical stress, MaxiLobe pumps can help extend service intervals and equipment life.
A robust gearbox design supports reliable performance under demanding conditions, reducing the risk of unplanned stoppages and supporting more predictable, resource-efficient operation and lower lifecycle costs.
MaxiLobe and MaxiLobe UltraPure pumps protect product quality and reduce cross-contamination risk through precision-profiled elastomers, superior cleanability and hygienic and high-purity design. MaxiLobe provides both EHEDG and 3-A certification alongside full FDA compliance as standard, delivering an uncompromised hygienic solution.
Every pump is factory-tested and supplied with a performance certificate confirming that it meets its specified operating curve before delivery, ensuring reliable commissioning and smooth startup.
MaxiLobe and MaxiLobe UltraPure are engineered for quick, predictable maintenance. Front-loading single seals can be replaced without removing the pump from the process line, reducing downtime during routine service. Interchangeable components and easily accessible shimming simplify servicing and help reduce maintenance time. Alfa Laval’s global service organization further supports maintenance wherever the pumps are installed.
Looking for a reprint of this article?
From high-res PDFs to custom plaques, order your copy today!